
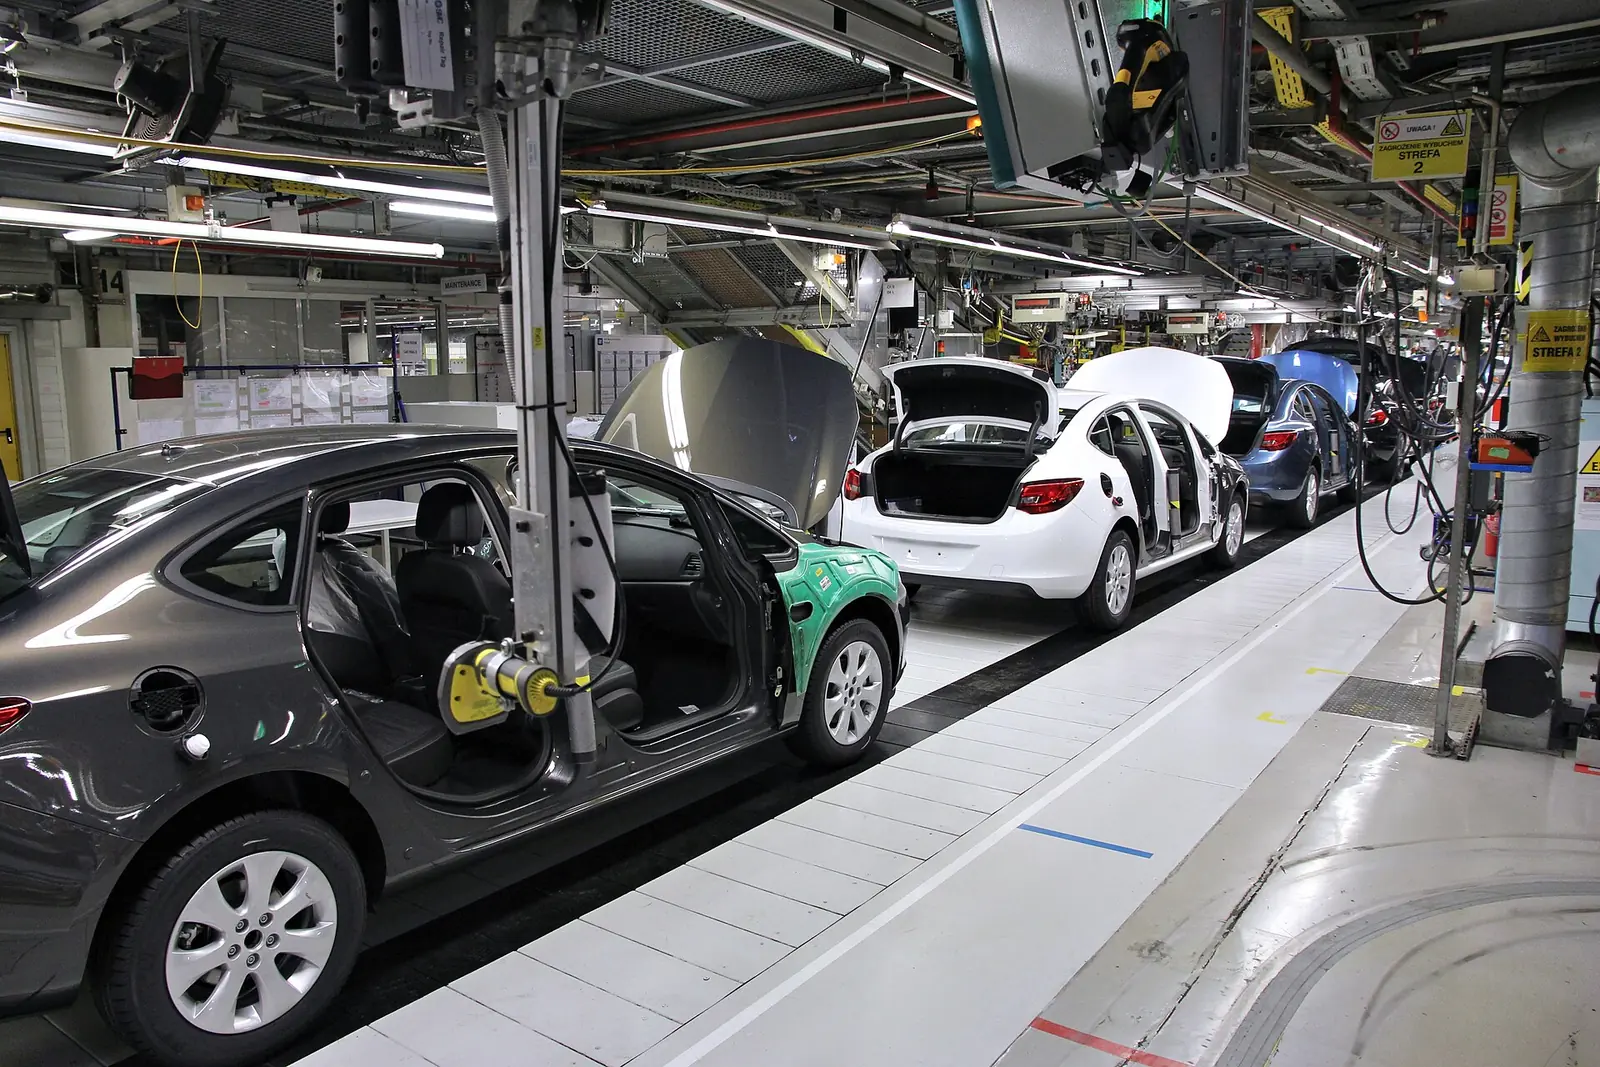
Automotive components and industrial manufacturing
Multi-level bills of materials, real shop-floor lead times, subcontracted operations, supplier quality that decides your own quality, and customers who audit your process.
The things we hear most in this trade.
- “Our plan says 60 minutes; the floor takes 225.
- “We changed a sub-assembly and forgot which parents it affects.
- “Job-work parts are on someone else's floor and on our books.
- “A supplier's bad lot became our customer's complaint.
Capability, and the outcome it buys you.
Queue, setup, run, wait and move time all modelled per step
the plan matches the floor.
Scrap cascades backwards through the routing
input is ordered for the real yield.
Overlapping steps — start the next operation after the first 5,000, not all 80,000
shorter lead times.
Multi-level recipes that explode to raw materials; "where used" answers which products are hit if a material is dropped; change one recipe and every parent is flagged cost-out-of-date
engineering change is controlled.
Swap a discontinued component across up to 50 recipes with a preview of the blast radius
obsolescence is a task, not a crisis.
Work centres with hourly cost, capacity, shift calendars, holidays, maintenance status and a fallback machine
capacity is real.
Job-work recipes with the vendor named; job-work challans that move custody without selling under Section 143; goods at the contractor stay on your books
subcontracting is native.
Supplier corrective-action requests, supplier scoring from acceptance rate and delivery, and formal qualification with expiry
supplier quality is your quality.
Quality checkpoints on each step with hold, rework, scrap or continue actions; control charts with 3-sigma limits and run rules; process capability trends
the process is measured.
Drawings, SOPs and supplier certificates attached to the recipe or the step and marked mandatory before production
the operator has the current drawing.
Work instructions in English, Hindi, Tamil and Gujarati on the same step
the floor reads its own language.
A bracket's routing has cutting, forming, plating (at a job-worker) and inspection. Plating goes out on a job-work challan; the parts stay on the books and show as physically at the plater. A supplier's steel lot fails hardness at incoming inspection; the lot is quarantined, a corrective-action request goes to the supplier, and their score drops. Engineering replaces a fastener across 31 recipes in one run with a preview; every parent is re-costed. The customer's auditor sees routing version 7 pinned to the batch.
The standards and regulations this industry answers to.
- IATF and ISO-style process control (SPC, Cpk)
- Customer PPAP-style documentation via attached drawings and certificates
- GST Section 143 job-work
- E-way bill
Talk to us about automotive & industrial.
Bring the hardest thing you have had to prove — the lot that failed, the return nobody could place, the audit that cost you a week. That is the demo.